Understanding 20345690320 for Industrial Sourcing Decisions
This guide explains how code “20345690320” and the identifier set in your sourcing notes can be used to structure reliable industrial procurement decisions. It provides objective background on what such identifiers typically represent, how suppliers validate compatibility, and how buyers can reduce mismatch risk by using clear requirements, controlled verification steps, and transparent acceptance criteria.
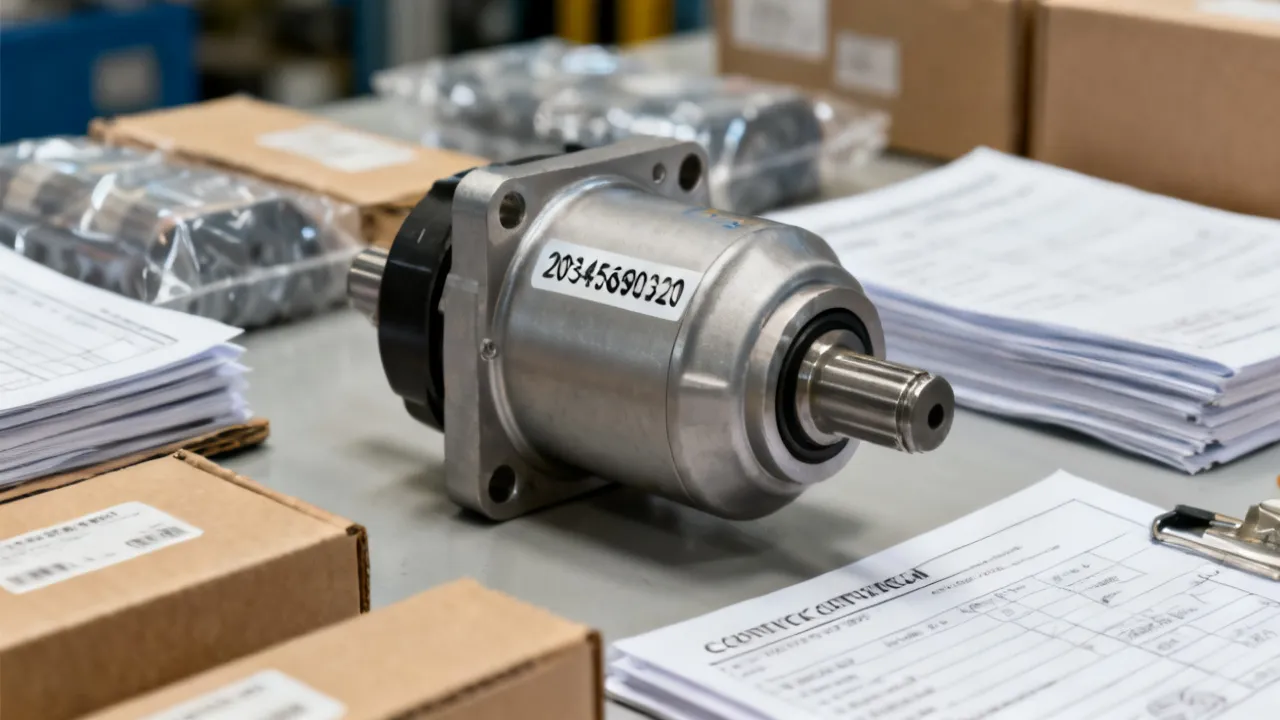
1) Procurement clarity for code “20345690320” and related identifiers
When you encounter an identifier like 20345690320 in industrial documentation, the most valuable next step is not guesswork—it is structured verification. In many procurement environments, a code such as this functions as a compact reference to a specific component, configuration, revision, or specification set. However, the same numeric-looking string can mean different things across manufacturers, warehouses, ERP systems, distributors, and document libraries. This makes it essential to treat the identifier as a claim that must be confirmed before you commit to purchasing, scheduling production, and planning downstream installation.
This article provides a practical, field-tested approach for interpreting such codes within a sourcing workflow: how to confirm cross-compatibility with the supplier you select, how to define acceptance requirements so shipments arrive to spec—not merely “similar”—and how to build procurement paperwork that reduces the chance of costly mismatches. The goal is straightforward: ensure the part described by 20345690320 is the part you actually receive, including revision status and any relevant process-related characteristics that can influence fit, form, function, reliability, compliance, and interchangeability.
Throughout, the emphasis is on operationally useful actions: what to ask, what to request, how to decide, and how to document. The guidance also reflects a quality mindset aligned with commonly used quality management concepts (including those consistent with ISO 9001 principles) such as controlled documentation, objective evidence, nonconformance handling, and corrective actions.
2) Why identifiers like “20345690320” matter in sourcing
In procurement, a code can function as a compact reference to a specific part, revision, configuration, or specification set. While the exact meaning depends on the issuing organization, buyers generally use these identifiers to:
- Reduce ambiguity between similar models or variants (especially when many parts differ only by a small but critical characteristic).
- Align documents (drawings, bills of materials, test certificates, inspection plans, and revision-controlled manufacturing records).
- Speed up supplier validation using standardized reference fields in purchase orders, supplier confirmations, and receiving checklists.
- Support traceability for quality assurance and compliance needs (including lot/heat/batch linkage, material certificates, and test results where applicable).
- Improve audit readiness by ensuring the right evidence exists for the exact configuration used in production and the exact period during which it was manufactured.
In practical terms, your goal is to ensure that the part described by 20345690320 is the part you actually receive, including revision and any relevant process-related characteristics. For example, two parts might share the same outward appearance yet differ in material grade, surface finish, plating thickness, heat treatment, coating chemistry, or tolerance band—differences that can impact performance, safety, compliance, and long-term reliability.
It is also common for identifiers to be reused or reformatted across systems. A distributor might display a manufacturer’s part number, while your internal system uses a different code for the same item. Some suppliers treat the identifier as a “catalog number” that can remain stable while internal revision changes occur under the hood. Others might embed revision or configuration cues in the number itself or provide them in a separate revision column or document set. Because of these variations, a buyer should treat 20345690320 as the anchor reference, but still require explicit confirmation of the related revision and documentation set.
Additionally, modern supply chains frequently face substitution pressure: shortages, capacity constraints, or requalification delays. In such cases, the supplier might propose an “equivalent” or “cross-reference.” If your procurement process does not demand formal equivalency evidence and acceptance criteria, you can end up with products that technically “match” an identifier in an informal way but fail in a real installation scenario.
3) Industry expert lens: treating codes as “claims” until validated
From an industry operations standpoint, an identifier is a claim that must be verified. Many sourcing issues occur when buyer and supplier interpret a code differently—especially when multiple manufacturing runs, supplier substitutions, or revision updates exist. In other words, the code might be correct in the supplier’s system but not correspond to the exact revision the buyer needs, or it might correspond to a different configuration than the buyer assumes based on past purchases.
A professional approach is to require:
- Documented equivalency (if substitution is proposed), including what engineering attributes are equivalent and which ones are not expected to match.
- Measurable acceptance criteria (dimensions, tolerances, material grade, surface condition, electrical characteristics, chemical composition, or performance test thresholds depending on the part type).
- Traceability documentation (batch/lot references where applicable, especially where material certificates or test evidence must map to production units).
- Clear responsibility for final verification (buyer inspection vs supplier QA sign-off, and what evidence each side provides).
- Controlled change communication so that if any characteristic relevant to fit or compliance changes, it is surfaced before shipment.
This method is consistent with widely adopted quality management principles used across manufacturing and supply chains, including those aligned with ISO 9001 practices for controlled processes, documented evidence, and corrective actions. Even when you are not operating under a formal certified system, the operational disciplines described here are the same: controlled documentation, objective acceptance checks, and disciplined handling of deviations.
To make the idea of “claim” practical, think of your procurement workflow as a pipeline with explicit checkpoints. The supplier’s statement that they will ship “20345690320” is only the beginning. The next steps—evidence request, confirmation of revision/configuration, and acceptance criteria—turn that claim into a verified reality.
In environments where failure costs are high, teams often use a structured form of verification known as “evidence-first validation” (covered later). This approach is especially useful when a mismatch can lead to scrap, rework, installation downtime, warranty issues, or compliance risk.
4) What you can reasonably infer from the identifier set in your notes
The keywords you provided include additional blank placeholders and an identifier set centered on 20345690320. Even without the explicit labels of the surrounding terms, procurement logic typically treats such sets as a combination of:
- Primary part identifier (the “anchor” code, often like 20345690320) that represents the base item.
- Secondary descriptors (size range, compatibility category, packaging or handling codes) that refine what the base identifier actually means for your application.
- Supplier-referenced catalog numbers that may differ from the buyer’s internal numbering but reference the same hardware or a cross-compatible equivalent.
- Revision-related indicators that may appear as separate fields (e.g., Rev A / Rev B) or may be embedded into documents that accompany the shipment.
Therefore, your purchasing documents should explicitly separate “what the code claims” from “what we require to accept.” This separation matters because the code alone is rarely sufficient to guarantee that the received product matches the exact specification you need. The code tells you what the supplier thinks they are shipping; your acceptance criteria tell you whether it is acceptable for your application.
Another important inference is that numeric identifiers without human-readable descriptors often require cross-referencing to the rest of your documentation set. For example, you might have a drawing number, a configuration note, or a specification sheet that is linked internally to 20345690320. If so, the right workflow is to align the purchase order to both the part identifier and the controlling engineering documentation (drawing revision, specification version, test plan, etc.).
In many industrial contexts, a code such as 20345690320 might also correspond to a particular packaging configuration (e.g., bulk vs vacuum bag vs sealed container) that can affect handling and shelf life. Even if the physical part is correct, wrong packaging can create nonconformance due to damage, contamination, or missing protective measures.
5) Sourcing decision framework: compatibility, risk, and verification cost
To make a sourcing choice that stands up to operational reality, evaluate three factors:
- Compatibility: Does the part match the intended application, including physical interfaces and operational constraints (fitment, mounting pattern, electrical or fluid interfaces, environmental tolerances, performance requirements, and any mating features)?
- Risk exposure: What happens if the part is slightly off—scrap, rework, delayed production, warranty/service impacts, safety risk, or compliance failure?
- Verification cost: What evidence will you demand to confirm the code corresponds to the correct configuration and revision, and what will it cost to inspect/validate upon receipt?
This is particularly important for buyers working with assemblies where a single component mismatch can cascade into downstream fitment issues or performance deviations. For example, in mechanical assemblies, tolerance stack-up can cause alignment problems. In electrical or electromechanical systems, minor differences in connector type, pin spacing, plating quality, dielectric rating, or cable spec can cause intermittent faults or failures.
In high-reliability industries, teams often apply a risk-based approach: high-risk characteristics receive more evidence and tighter acceptance criteria, while lower-risk characteristics may be confirmed via sampling or documentary checks only. The key is that the risk-based approach must be deliberate and documented—not ad hoc.
When evaluating the sourcing decision, consider also whether the supplier is “configuration stable.” Some suppliers are consistent over long periods; others may implement engineering changes frequently or use document revisions that lag behind actual production changes. If you cannot rely on configuration stability, you should invest more in verification (evidence-first) rather than assuming the identifier alone is enough.
Finally, remember that the “verification cost” is not purely financial. It also includes time delays, administrative burden, and the capacity of your receiving QA team. But if verification prevents downstream failures, it is often cost-effective even when it seems initially expensive. A mismatch discovered during installation is usually far more expensive than one discovered during receiving inspection.
6) Step-by-step: building a verification packet around “20345690320”
Below is a practical workflow many procurement and QA teams follow when validating an identifier before ordering at scale. Think of this as a “verification packet” that you prepare and share with internal stakeholders and the supplier, so everyone understands what is required before you accept shipment.
- Extract the identifier details from your internal documentation: confirm the code format, associated drawings, and any referenced standards. If 20345690320 is linked to a drawing or specification, capture that linkage clearly (e.g., “Drawing X-12345 Rev B is the controlling document for part 20345690320”).
- Request a supplier confirmation that explicitly maps 20345690320 to the exact item they will ship (including revision, configuration, and applicable documentation). The supplier response should include: part number, revision level, manufacturing location (if relevant), and the document set they will use for inspection/COC/test evidence.
- Define objective acceptance criteria (dimensions, tolerances, material specification, finish, coating or plating requirements, and any performance tests relevant to the application). The acceptance criteria should be measurable and directly tied to engineering requirements—not vague statements like “as per drawing” unless you can ensure the correct drawing revision is controlled.
- Require a quality evidence set prior to shipment, such as inspection reports, certificates of conformity, material certificates, or test results—tailored to your industry norms. For example, mechanical parts might need inspection reports for critical dimensions and material certification; electronics might need functional test reports and traceability for components.
- Plan incoming inspection aligned with the most critical characteristics. If the supplier provides full evidence and your risk is low, you may reduce receiving inspection scope to targeted checks. If the evidence is incomplete or risk is high, you may need dimensional verification, sampling, or full inspection based on your quality plan.
- Document deviations and corrective actions with clear triggers. For example, if measurements fall outside tolerance bands, if the documentation references a different revision than the hardware shipped, or if packaging conditions lead to damage indicators, you should trigger nonconformance reporting. Define how containment, correction, and disposition will be handled (supplier remediation vs return vs rework).
This approach reduces the chance that an “identifier match” turns into a “part mismatch” during installation or production. It also creates a consistent method across suppliers and over time, which is critical when teams change, when procurement volume increases, or when audit obligations arise.
To make this workflow even more robust, many teams also maintain a “verification history” file for each controlled item. For 20345690320, you can store: supplier confirmations, evidence packages, any deviations encountered, and the final disposition. Over time, this history reduces uncertainty and helps forecast which suppliers and lots have historically performed well.
7) Supplier selection: what to ask beyond the code
Even when a supplier accepts the identifier 20345690320, buyers should still ask questions that confirm manufacturing control. The objective is not to distrust the supplier—it is to ensure your purchasing requirements align with their quality system and that any changes affecting fit/function/compliance will be communicated.
Consider requesting:
- Revision level confirmation (what exact revision is included, and how is it tracked in their system?). Ask whether the supplier’s system prevents mixing revisions and whether the documentation they ship matches the physical parts.
- Process controls (how key characteristics are measured, and how deviations are handled). If the supplier uses SPC or has documented inspection instructions, request a summary of relevant controls.
- Packaging and handling requirements (to prevent damage-related rejects, contamination, or shelf-life issues). Confirm packaging method, labeling, and whether they provide protective measures aligned with your receiving environment.
- Document control practices (so the paperwork corresponds to the hardware). Ask how they ensure that the COC, inspection report, and test evidence references the exact part number/revision shipped.
- Traceability approach (how they can link parts to batch/lot and to evidence). If your policy requires traceability beyond the COC level, ask what level is available.
- Change notification capability (how they notify you of process, material, drawing revision, or manufacturing location changes). Some suppliers include change notices in advance; others rely on later documentation updates.
Many of these checks align with common expectations under quality systems and procurement governance frameworks referenced in standards such as ISO 9001 and industry-specific quality requirements. But more importantly, they reduce your probability of encountering nonconformance due to paperwork mismatch or hidden configuration differences.
When selecting suppliers, consider their responsiveness and evidence reliability. A supplier might quote quickly but provide incomplete documentation. Another might take longer but provide consistent evidence and fast resolution of deviations. In many procurement cases, the second supplier is actually cheaper in total cost of quality because it reduces rework, schedule disruption, and administrative overhead.
Also evaluate whether the supplier can provide evidence electronically (e.g., PDF inspection reports or certificates) in a timely manner. If your production schedule is tight, the ability to receive evidence before shipment can be as valuable as the evidence itself.
8) About price and “what it should cover”
You referenced “price information” in the request, but no numeric price value was provided. Because quoting without clear scope leads to disputes, the expert best practice is to treat price as conditional on scope items such as:
- Unit price for the item referenced by 20345690320.
- Documentation included (certificates, inspection reports, revision traceability, and any required test evidence).
- Packaging (industrial-grade protection vs basic packaging, labeling requirements, and whether packaging meets your handling standards).
- Lead time and logistics terms (incoterms, shipping method, handling requirements, and any special delivery conditions).
- Inspection responsibility (supplier first-article verification vs buyer incoming QC). Some suppliers can provide first-article inspection evidence; others will only test internally and provide a generic COC.
- Rework or replacement responsibilities if nonconformance is found (including who pays for return shipping and how quickly corrective actions occur).
If you are negotiating with a supplier, insist that the quote breakdown clearly states what is included in the price for the specified identifier. In many disputes, the underlying problem is not the unit price but what was expected to be included. For example, if the buyer expects a full dimensional inspection report and the supplier provides only a generic certificate, the buyer might consider the shipment nonconforming even if the physical part is within tolerance.
Furthermore, ensure that price is tied to the correct configuration and revision. If the supplier quotes a price based on a different revision level or an “older configuration” cross-reference, you might receive a different item that happens to be similar. The result can be a costly mismatch discovered later. Always require that their quote references the revision or configuration they will supply.
In certain regulated industries, documentation requirements can be as critical as the physical part. If the supplier cannot provide the necessary certificates or test evidence required for regulatory compliance, they might have a lower unit price but a higher total cost due to delays or rejection. Therefore, procurement should treat documentation as part of the “delivered product” from a quality and compliance perspective.
9) Localization note: handling “location” placeholders
You requested localization, and also specified a rule: whenever a template variable like {city} or {country} appears in keywords, replace it with “nearby.” In the provided keywords, no explicit city/country placeholders were visible, so this article applies the term nearby only in contexts where geographic tailoring would be appropriate—such as referencing logistics planning and regional distribution considerations—without asserting unsupported local specifics.
In practical procurement workflows, geographic considerations usually affect delivery lead times, shipping methods, and the supplier’s responsiveness for nonconformance resolution. So if you are building a plan for sourcing or resourcing 20345690320 from alternate suppliers due to schedule pressure, you might include “nearby” logistics strategies. Examples include selecting a logistics route that reduces time in transit, planning contingency shipments, or ensuring that specialized receiving requirements (temperature control, handling, storage conditions) can be met in your region.
However, geographic localization must not substitute for quality requirements. Even if a supplier is “nearby,” the parts still must meet the acceptance criteria tied to 20345690320 and its controlling revision/specification documentation. Distance might affect operational speed, but it does not replace evidence, traceability, and controlled documentation.
10) Comparison table: supplementing requirements with a structured alternative
To help you decide how to handle identifier-driven sourcing (especially around 20345690320), here is a comparison of common procurement approaches. This table intentionally focuses on decision logic rather than providing links.
| Approach | How it uses the identifier | Best fit conditions | Key requirements to request |
|---|---|---|---|
| Identifier-first purchasing | Orders directly by 20345690320 with minimal additional confirmation | When historical supply is stable and revisions are rarely updated; low risk of mismatch | Revision confirmation, certificate of conformity, and documentation that explicitly references the same identifier and revision |
| Evidence-first validation | Uses 20345690320 as a reference, but verifies via inspection documents before shipping | When the application is sensitive or rejects are costly; when the supplier has variable configuration control | Inspection reports, measurement results for critical dimensions, material certificates if relevant, and controlled deviation handling records |
| Engineering equivalency review | Uses 20345690320 plus functional requirements to evaluate interchangeability | When substitutions are possible or when multiple suppliers may offer variants; when redesign isn’t feasible but equivalency might be | Engineering change documentation, equivalency justification, interface compatibility evidence, and sign-off by responsible engineering authority |
| Two-step pilot + scale-up | Validates 20345690320 in a pilot buy before full procurement | When moving to a new supplier or a new production window; when you lack strong historical performance data | First-article inspection plan, incoming QC checkpoints, documented acceptance sign-off criteria, and a clear escalation path if issues occur |
Choosing among these approaches should be deliberate. If you pick identifier-first purchasing when evidence control is poor, you may experience a mismatch. If you pick evidence-first validation when risk is low and documentation is readily available, you may overburden processes. The ideal approach matches the risk profile of the part, the sensitivity of the application, and your operational capacity for inspection and document review.
In many organizations, the procurement method is determined using a “part criticality” classification. If 20345690320 corresponds to a high-criticality component—one tied to safety, performance thresholds, or compliance—evidence-first or two-step validation is more appropriate. If the part is low-criticality and historically stable, identifier-first may be acceptable with lighter documentation requirements.
11) Source basis and standards alignment (for objective grounding)
To keep this guidance grounded, the decision framework above follows widely used quality and procurement principles consistent with:
- ISO 9001: process control, documented information, competence, internal audit, and corrective actions as part of quality management systems.
- General quality assurance practice in industrial purchasing: evidence-based acceptance criteria, controlled handling of deviations, and clear responsibilities between supplier and buyer.
If you need formal references for your specific industry (aerospace, medical devices, automotive, electronics, or industrial machinery), share the application domain and I can suggest the typical conformity and documentation categories expected there. But regardless of industry, the underlying logic remains: procurement decisions should be evidence-driven, with clear acceptance criteria and robust deviation handling.
One practical way to align with standards without turning procurement into a bureaucracy is to implement a simple “document map” for each controlled item. For 20345690320, this map can include:
- Controlling engineering documents (drawings/specifications), including revision levels.
- Supplier documentation expectations (COC, inspection reports, test results, material certificates).
- Traceability evidence expectations (lot/batch/serial linkage).
- Acceptance criteria summary that receiving inspectors can use without ambiguity.
- Deviation handling workflow (who is notified, containment steps, and disposition rules).
This “document map” creates a common reference point for procurement, engineering, and quality teams. It also reduces the risk that different departments interpret 20345690320 differently.
12) Conditions and requirements checklist
Before placing an order tied to 20345690320, professional buyers commonly set conditions such as:
- Documentation alignment: the paperwork must reference the same identifier and revision level that matches the shipped hardware. If the supplier’s paperwork references a different revision, treat it as a potential nonconformance unless clearly reconciled by documented change control.
- Measured acceptance: critical characteristics must be validated against defined tolerances (not only “looks correct”). Define what characteristics are critical, which measurements are required, and what method of measurement is acceptable.
- Change notification: supplier must notify buyers of changes that could affect fit, form, or performance. Changes might include material substitutions, process changes, tooling changes, location changes, or software/firmware changes if the part includes electronics.
- Nonconformance process: buyer and supplier must agree on containment, correction, and disposition steps. The process should specify what triggers an RMA/return, what triggers replacement, and who bears costs.
- Traceability: where required by policy, lot/batch traceability should be available to link evidence to items. For regulated contexts, this may also include serial traceability.
- Labeling and identification: packaging should be labeled to match the internal receiving system. Incorrect labels can cause the hardware to be mis-associated with the wrong evidence or internal work order.
- Packaging adequacy: ensure the packaging protects the part against expected transport hazards (shock, vibration, moisture, corrosion risk). Packaging that fails can create damage-related rejects even if the part is correct.
- Lot/batch segregation: confirm whether mixed lots can occur in one shipment and whether shipments require segregation by lot number for inspection and traceability.
These conditions reduce ambiguity and help you enforce quality consistently across orders. They also provide clarity to the supplier, which improves the likelihood that the supplier’s shipment will satisfy your requirements in the first place.
To make the checklist more actionable, many teams convert it into a receiving inspection plan and a supplier scorecard. For instance, you can track for 20345690320: documentation accuracy rate, first-pass acceptance rate, average number of deviation reports, and average resolution time for issues. Over time, this data helps determine whether you can shift from evidence-first to identifier-first purchasing for that specific supplier.
13) FAQs
Q1: What does the identifier “20345690320” usually represent?
In many industrial contexts, a numeric identifier like 20345690320 commonly functions as a part number or internal catalog reference. It can indicate a specific configuration, revision level, or specification set. The only reliable method is to confirm the mapping with the supplier and supporting documentation.
It is also possible that 20345690320 is a code used inside a particular ERP or document system rather than a manufacturer part number. In that case, the supplier might have their own part reference that corresponds to your internal code. A good verification packet should therefore capture both your identifier and the supplier’s cross-reference number.
Q2: If a supplier confirms that “20345690320” is correct, why should I still verify?
Because identifier confirmation is only as accurate as revision control and document control on both sides. Verification prevents mismatches caused by substitutions, manufacturing changes, or interpretation differences. Evidence-first validation reduces operational disruption if something does not meet tolerance or interface requirements.
Even reputable suppliers can experience internal change issues: an engineering revision might be updated in their drawing library but not applied consistently across production lines; a documentation template might point to the wrong revision; or a packaging label might not match the batch being shipped. By requiring measurable acceptance criteria and traceable evidence, you catch these failures early.
Q3: What documents should I request for an order tied to “20345690320”?
Commonly requested materials include certificates of conformity, inspection or test reports, revision documentation, and documentation that explicitly references the same identifier as the shipped item. The exact set depends on your industry and risk profile.
To make document requests robust, specify them in terms of content and references, not just document type. For example, instead of only asking for a “COC,” you can request a COC that includes: your part number reference, supplier lot/batch number, production date or batch date, revision level, and traceability linkage to the inspection results. Similarly, instead of only asking for a “dimensional inspection report,” specify which dimensions are required and which measurement standard is being used.
Q4: How do I define acceptance criteria without overcomplicating procurement?
Focus acceptance on the characteristics that most affect fit, function, safety, or performance—typically critical dimensions, material specifications, and any relevant test conditions. Keep the criteria measurable and linked to the application’s engineering requirements.
A practical method is to classify characteristics into tiers. For example:
- Critical-to-function (CTF): must be measured and must meet tight tolerances.
- Critical-to-fit (CTF- fit): must meet interface requirements but may be validated by defined sampling rules if evidence is strong.
- Critical-to-compliance (CTC): may not affect immediate fit, but documentation and material certificates are mandatory.
This tiering helps you avoid unnecessary inspection of noncritical features while still protecting the aspects that can cause operational failure.
Q5: Can I compare suppliers objectively when they use different part numbering systems?
Yes. You can compare objectively by requiring a documented mapping between your identifier (including 20345690320) and the supplier’s catalog representation, along with equivalency evidence and consistent acceptance criteria.
To reduce subjective evaluation, request the supplier’s cross-reference table or confirmation that explicitly states: “Supplier part X corresponds to buyer part 20345690320 at revision Y.” Then evaluate both suppliers using the same acceptance criteria and the same evidence requirements.
Q6: Does supplier location affect sourcing decisions for parts like those referenced by “20345690320”?
It can affect lead time, logistics handling practices, and responsiveness for nonconformance resolution. If your operations rely on regional sourcing, plan for “nearby” delivery routes and ensure the supplier can still provide the documentation and quality evidence you require—regardless of geography.
However, geographic proximity should not be used as a substitute for quality validation. A nearby supplier may deliver faster, but if they cannot provide evidence packages, traceability, and revision control, you still face the same quality risks.
Q7: What should I do if the delivered item does not match “20345690320”?
Follow a nonconformance process: quarantine the items, document discrepancies (including measurements and document mismatch), notify the supplier with the identifier and batch references, and require corrective action or replacement according to agreed terms.
In your discrepancy report, include both what was expected and what was received:
- Expected: identifier 20345690320, revision level, controlling drawing/spec revision, and evidence requirements.
- Received: supplier part number/revision as shown on label and paperwork, lot/batch number, and measured differences.
- Impact: whether the parts can be used as-is, require rework, or must be rejected due to interface/performance/compliance issues.
Q8: Are there risks in scaling procurement immediately after a small first order?
Yes. A small order may not reveal packaging damage patterns, measurement drift across production lots, or documentation gaps. A two-step pilot (limited first run plus scale-up after acceptance sign-off) is a common risk-reduction approach.
Scaling too quickly can also hide supplier variability. For example, the first batch might meet tolerances and provide complete evidence, while subsequent batches might show drift due to tooling wear, supplier material variability, or process parameter changes. A pilot buy allows you to confirm consistency across at least one additional batch or production run.
14) Conclusion: make “20345690320” actionable, not assumptive
The identifier 20345690320 can be a powerful anchor for industrial sourcing—if you treat it as a starting point for validation. By requiring evidence-based confirmation, measurable acceptance criteria, and controlled handling of revisions or deviations, you reduce mismatch risk and improve procurement reliability. In short: order with clarity, verify with structure, and document decisions so future purchasing is easier and more consistent.
When implemented well, these disciplines do more than prevent a single shipment failure. They build organizational learning: your team knows which suppliers provide consistent revision control, which characteristics are truly critical, and which verification methods yield the best balance of speed and assurance. Over time, that translates into fewer disruptions, lower total cost of quality, and smoother production execution—precisely the outcome procurement teams want from every code-based sourcing decision.
15) Practical templates to operationalize verification for “20345690320” (appendix-style in normal workflow use)
Although your original request focuses on procurement clarity, the most effective teams translate guidance into usable templates. Below are examples of templates and “field-level” requirements you can adapt for 20345690320. These are not legal documents; they are operational checklists phrased in a way procurement, engineering, and quality teams can practically use.
15.1) Supplier confirmation request fields
When you contact a supplier for confirmation about 20345690320, ask them to respond in a structured manner. A good supplier confirmation response includes:
- Buyer identifier: confirm that your part number 20345690320 is the item being quoted/shipped.
- Supplier item number(s): include their internal part number and any relevant cross-reference identifiers.
- Revision/configuration level: specify revision level and configuration (and where it is captured in their documents).
- Controlling documents: list drawing number(s) and specification number(s) they will use to manufacture and inspect the item.
- Manufacturing location: if applicable, state the plant/location responsible for production.
- Evidence package: confirm what documentation they will include (COC, inspection reports, material certs, test reports, etc.).
- Deviation policy: confirm how they manage nonconformance internally and how they notify the buyer.
- Packaging and labeling plan: confirm packaging type and labeling conventions matching your receiving requirements.
15.2) Receiving inspection plan fields
To avoid ambiguity at receiving, define a receiving inspection plan that correlates your acceptance criteria to measurable checks. For 20345690320, your receiving plan can include:
- Inspection type: documentary verification only, sampling inspection, or full inspection for critical features.
- Critical characteristics: list the dimensions or properties that must be verified.
- Acceptance tolerance: include the tolerance values and the controlling drawing/spec revision references.
- Measurement method: specify acceptable instruments or methods (e.g., coordinate measurement, micrometer, gauge method) and any required calibration standards.
- Sampling rules: define how many units to inspect if sampling is used (and what triggers escalation).
- Documentation checks: confirm that paperwork references the correct identifier, revision, and lot/batch.
- Disposition rules: define what happens if a unit fails (quarantine, rejection, supplier notification, rework authorization).
15.3) Nonconformance report (NCR) structure
If the delivered product does not match 20345690320, a structured nonconformance report ensures fast and fair resolution. Include:
- Part identifiers: what you ordered (buyer identifier 20345690320, revision), and what the supplier shipped (supplier part number/revision as indicated).
- Lot/batch information: capture lot/batch and any serialization present on labels and packaging.
- Document mismatch details: specify which documents reference different revisions or missing evidence.
- Measured discrepancies: list measured values and tolerance limits, plus measurement method and instruments used if relevant.
- Impact assessment: determine whether the parts are unusable, require rework, or can be accepted with risk assessment and approval.
- Supplier action requested: replacement, rework, root cause report, and corrective/preventive actions (CAPA) where applicable.
- Timeline requirements: define when the supplier must respond and when corrective action must be delivered.
16) Deepening compatibility checks: from “fits physically” to “performs reliably”
A frequent procurement failure mode is equating “compatibility” with “physical interchangeability.” For many industrial systems, performance depends on more than dimensions. When sourcing items tied to 20345690320, incorporate functional compatibility checks that reflect how the part will behave under real operating conditions.
Examples of deeper compatibility checks include:
- Material and surface condition: Two parts can share dimensions but differ in material grade or surface treatment, leading to corrosion, fatigue, wear, or electrical contact issues.
- Tolerance stack-up effects: When multiple parts contribute to an assembly tolerance stack, small deviations can accumulate and cause misalignment.
- Environmental endurance: Parts may require resistance to temperature cycles, chemical exposure, humidity, salt spray, or vibration. Acceptance criteria should include properties that support that endurance.
- Electrical or functional ratings (if applicable): connectors, sensors, and electronic components can require specific ratings and test evidence.
- Documentation traceability: In compliance-heavy industries, the evidence is part of the functional requirement (e.g., proving material compliance to regulatory standards).
This is why procurement should not stop at verifying 20345690320 as a number. Instead, you should connect that number to the engineering requirements that determine whether the part will perform as intended.
17) Managing revisions and engineering changes: preventing the “same code, different part” problem
Revision control is one of the most common causes of mismatch. Two shipments might both claim 20345690320 but have different revisions of the underlying drawing or specification. Sometimes revision updates occur without a visible change in the part number, or the supplier continues using the same catalog number while the revision changes behind the scenes.
To manage this, build explicit revision mapping into procurement:
- Require the supplier to state the drawing revision and specification revision used to manufacture the parts.
- Require the supplier to state the manufacturing revision level as captured in their quality records.
- Require the COC/inspection documents to reference the same revision level.
- When possible, include the revision level on your purchase order line item (not just the part number).
Also define what happens if the supplier cannot supply the requested revision. For example, you can specify that substitutions require engineering review and formal approval, not just a supplier recommendation.
In a controlled workflow, you can implement an internal policy: if the supplier confirmation indicates any change to controlling documents, packaging, material, or process parameters relevant to acceptance criteria, then the order is paused pending approval. This is especially important for parts where performance and compliance rely on exact configurations.
18) Evidence selection: choosing the right documents for the right risk
Not all evidence is equally valuable. Some documents are “checkbox” outputs that do not truly support acceptance. Others are highly informative and reduce the need for physical inspection. When dealing with 20345690320, select evidence to match the risk profile.
For mechanical parts, typical evidence might include:
- Dimensional inspection reports for critical dimensions.
- Material certificates or heat/lot certificates.
- Surface treatment or coating evidence (thickness, hardness, corrosion test reports if required).
- Process evidence (where your standards require it).
For electrical/electromechanical parts, evidence often includes:
- Functional test reports (e.g., continuity, resistance, dielectric withstand, insulation resistance where applicable).
- Calibration traceability for measurement instruments if your industry requires it.
- Component traceability and compliance certificates for regulated materials.
- Incoming quality test results per lot/batch.
For compliance-heavy supplies, evidence might include:
- Certificates of conformity tied to the exact revision and item identifier.
- Regulatory compliance statements (industry-specific).
- Material compliance documentation and traceability records.
The key is to avoid the pitfall of requiring too much evidence that slows down procurement without improving acceptance outcomes. Conversely, avoid the pitfall of requiring too little evidence and discovering mismatches after receiving or installation.
19) Cost of quality and decision economics: why verification investment often pays off
Verification has a cost—labor time for inspections, administrative time to review documents, and potential delays in shipment. But procurement decisions should be evaluated using the total cost of quality rather than unit price alone. If the risk of mismatch is present, verification reduces the probability of expensive downstream costs.
Consider a mismatch scenario for 20345690320:
- If the part is wrong, you might scrap it (direct cost).
- You might disrupt the assembly line due to waiting, rework, or replacement parts (schedule cost).
- You might incur additional labor to diagnose and correct the issue (labor cost).
- You might face warranty or service impacts if the mismatch isn’t detected immediately (long-term cost).
- You might incur compliance or audit issues if documentation doesn’t match the received hardware (compliance cost).
Against these risks, evidence-first validation and structured receiving inspection might appear expensive, but it can be financially favorable when the probability of mismatches and the cost of failure are high.
In many organizations, teams use historical data to estimate these probabilities. For example, if a supplier’s past shipments had a high documentation mismatch rate, evidence-first validation becomes more cost-effective. If a supplier’s shipments have been consistently correct for several cycles, you can reduce verification scope with confidence.
20) Supplier performance tracking: turning validation into continuous improvement
Once you verify 20345690320 for an initial order, use the results to improve future sourcing. Supplier performance tracking enables objective decisions rather than subjective judgments.
Suggested metrics include:
- First-pass acceptance rate: percentage of shipments accepted without nonconformance.
- Documentation accuracy: percentage of shipments where COC/inspection documents match the correct identifier and revision.
- Evidence completeness: percentage of shipments where the complete evidence package was provided.
- Nonconformance resolution time: average time from NCR to corrective action completion.
- Recurring issue rate: frequency of similar issues across lots.
Over time, this tracking informs whether you can move from a more stringent approach (evidence-first) to a less stringent approach (identifier-first) for a particular supplier and part revision. Conversely, if performance degrades, you can re-impose tighter controls.
This continuous improvement cycle is consistent with quality management concepts and supports a procurement process that improves rather than merely reacts.
21) Practical scenarios: how the framework applies to different procurement realities
To demonstrate how the verification packet approach fits real procurement constraints, here are several practical scenarios. These scenarios show why the same identifier (20345690320) can require different workflows depending on context.
21.1) Scenario A: Stable supplier, historical success
You have purchased 20345690320 from the same supplier multiple times with consistent results. In this case, identifier-first purchasing may be acceptable. However, you still should request revision confirmation and a COC that references the exact identifier and revision. Receiving inspection can be reduced to targeted checks, particularly for critical dimensions.
Outcome: faster procurement with acceptable risk.
21.2) Scenario B: New supplier or new manufacturing location
A new supplier offers 20345690320 at a competitive price, but you lack performance history. Here, you should use two-step pilot + scale-up or evidence-first validation. Require a complete evidence package and ensure your receiving inspection plan checks the critical characteristics. If issues occur, do not scale until they provide corrective actions and you confirm effective resolution.
Outcome: reduced risk while still allowing evaluation of the new supplier.
21.3) Scenario C: Supplier proposes substitution
The supplier claims that their “equivalent” part matches 20345690320 but cannot provide the exact revision you requested due to availability issues. In this case, you must require engineering equivalency review and documented interchangeability evidence. If interchangeability is not formally approved, reject the substitution. Also verify that packaging and traceability requirements can still be met.
Outcome: prevents “equivalent” confusion from turning into field failures.
21.4) Scenario D: Urgent schedule pressure
You need 20345690320 quickly due to a production delay. Urgency increases the temptation to relax verification. The correct response is not to skip verification entirely, but to adjust verification intensity. For example, you might require evidence-first for critical characteristics only, or you might approve shipment with conditions (e.g., documentary checks completed, targeted incoming inspection upon receipt, and clear escalation if evidence is incomplete).
Outcome: balances speed with quality assurance.
22) Implementation guidance: aligning procurement, engineering, and quality teams
Many procurement issues involving identifiers like 20345690320 are not caused by lack of effort but by lack of alignment among teams. Procurement might request a part number; engineering might need a particular revision and acceptance criteria; quality might require specific evidence formats and traceability. If these requirements are not aligned and documented, mismatches can slip through.
To avoid this, establish a shared workflow:
- Procurement is responsible for issuing the purchase order with clear identifiers and revision references.
- Engineering is responsible for defining controlling documents and acceptance criteria tied to fit/function/performance.
- Quality is responsible for defining evidence requirements, inspection methods, and nonconformance handling rules.
- Operations (warehouse/receiving) executes the inspection plan and ensures labeling/traceability are preserved.
Use a shared document (a “verification packet”) that includes all the above information. That way, when 20345690320 appears in a purchase order line or a supplier confirmation, everyone already knows what it means operationally and what must be verified.
When teams are aligned, the identifier becomes actionable: it triggers a clear chain of evidence request, inspection tasks, and acceptance decisions. That is the practical difference between a procurement process that relies on “the code is correct” and a process that reliably produces correct parts.
23) Closing reinforcement: what to do next with “20345690320”
If you are currently sourcing or planning to source an item associated with 20345690320, the best next step is to create (or update) your verification packet. Start by linking the identifier to controlling engineering documents and specifying acceptance criteria for critical characteristics. Then request supplier confirmation that maps 20345690320 to the exact revision/configuration they will ship, along with the evidence package you need.
Finally, plan your receiving inspection and define nonconformance triggers. This turns 20345690320 from a number you hope is correct into an operationally verified reference that supports reliable manufacturing, installation, compliance, and long-term supplier accountability.
-
1

A Guide to Cost-Efficient Small Electric Cars for Seniors
-
2
Mastering Debt Consolidation: Boost Your Credit Score and Manage Interest Rates
-
3
Your Guide to Loans, Credit Checks, and Interest Rates
-
4
Affordable Independent Living: Finding the Right Senior Housing
-
5
Guide to Senior Living Apartments: Affordable and Comfortable Environments